buyer guide
Volume Ramp Planning for Stand Mixer Bowl OEM Programs
Send your drawing for DFM review
Even a rough print, target volume, and finish requirement are enough for a go/no-go and next-step reply within one business day.
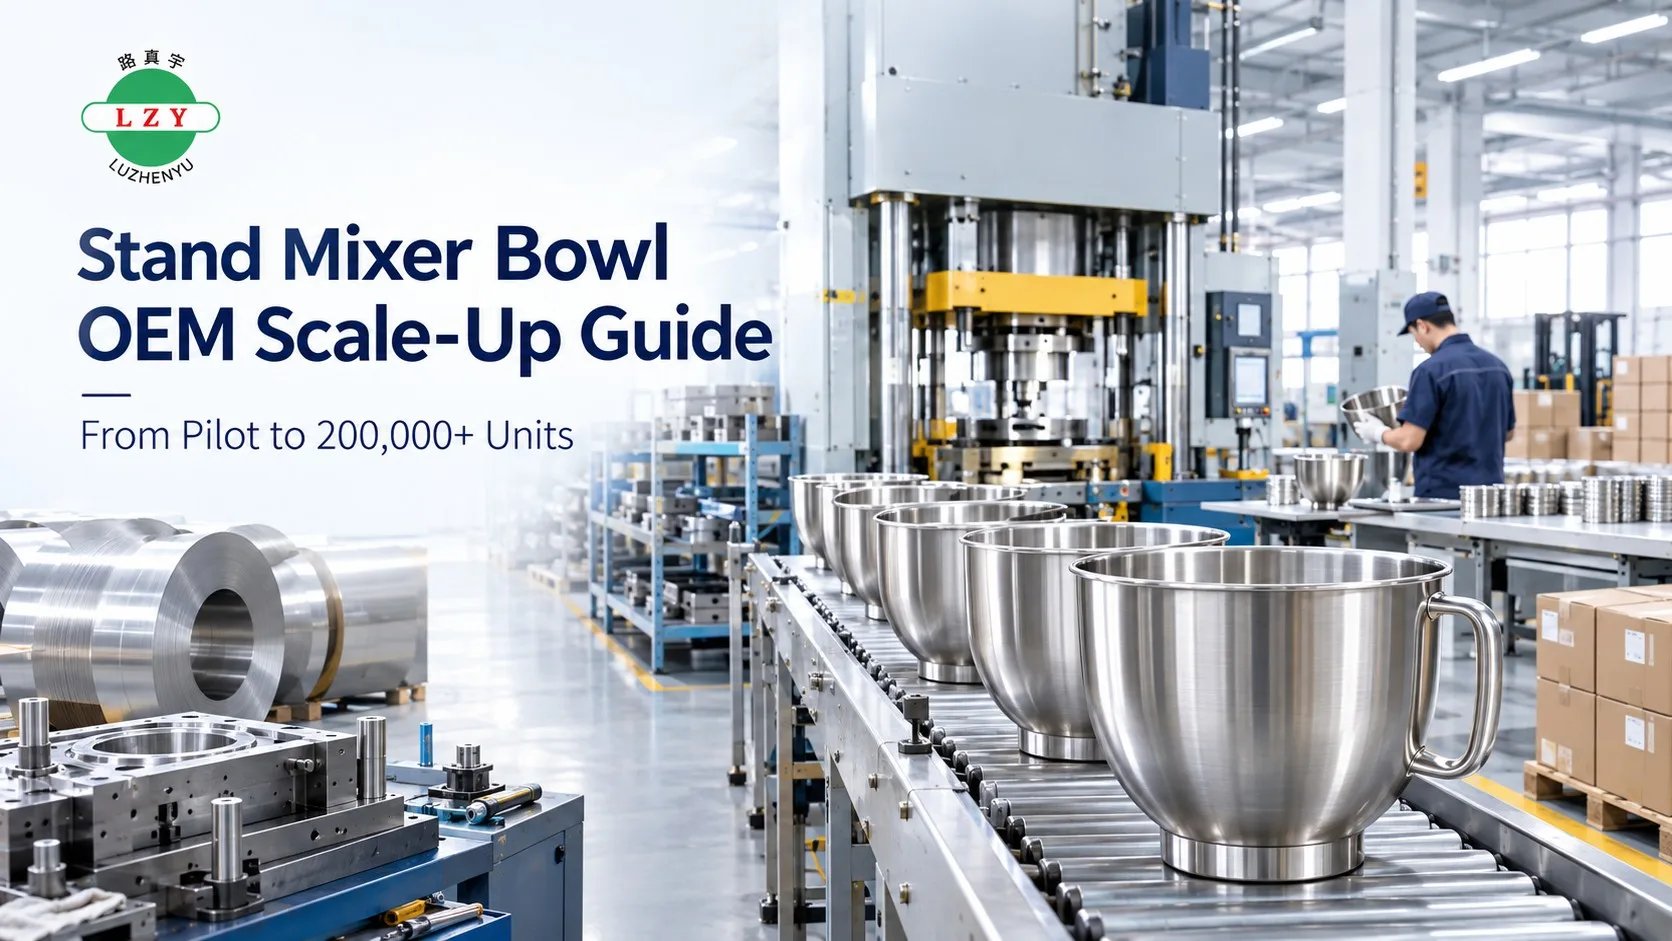
Volume ramp fails when pilot success is assumed to scale linearly without mold PM schedule, coil contracts, pack capacity, or QC headcount plan. Stand mixer bowl programs targeting high monthly output—250,000+ stand mixer bowls produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output class across supplier portfolio—need ramp curves, maintenance windows, and forecast update rhythm charted before volume PO release.
Ramp curve: avoid step to full MOQ day one
Gradual increase over 4–12 weeks: week 1 at 30% target line speed, week 4 at 70%, week 8+ at 100% after IPQC Cpk stable. Step change without line proof spikes cosmetic scrap and hub gauge failures when operators accelerate before patrol intervals adjust.
Mold PM aligned to ramp milestones
Schedule trim/punch PM at defined piece counts—align with ramp milestones not calendar guesswork. Punch radius wear shows as hub drift before catastrophic failure. Luzhenyu tracks PM across 60+ owned and customer-funded tooling managed under project agreements—buyers should require PM log access for high-volume programs.
Coil supply and allocation
Secure coil allocation for locked grade and thickness—ramp stalls on material shortage or wrong heat mechanical properties. IQC must gate new heats before acceleration week. See 304 vs 201 guide.
QC scaling before speed
Increase IPQC headcount or tighten patrol interval before line speed max. Cosmetic yield collapses when polish stations starved or packing line backs up causing dent damage. OQC sampling plan may require 100% hub gauge until steady state.
Pack and logistics capacity
Retail inner pack and master carton throughput must match bowl output—ramp includes pack line, not only press. Drop test failures at higher pack volume indicate design change needed before export.
Buyer forecast rhythm during ramp
Weekly output review first 8 weeks: actual vs plan, scrap PPM, OTIF partials. Adjust forecast PO releases based on ramp data—not original launch spreadsheet alone.
Luzhenyu Hardware operates from its Dongguan production base in Chashan Town, Dongguan, Guangdong, with project-matched forming presses. Stand mixer bowls represent a major share of customer programs, with 250,000+ stand mixer bowls produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output. The factory manages 200+ tooling development references across customer projects and customer-funded tooling managed under project agreements under project agreements. Quality workflow follows IQC → FAI → IPQC → OQC; certification status and scope should be verified separately. See about Luzhenyu and deep drawing capability for factory context.
Repeat OEM bowl programs depend on sequential gates—not a final inspection alone. IQC verifies incoming coil grade, gauge, and mill certificate match. FAI locks dimensions after die setup or material change. IPQC patrols rim, hub, wall thickness, and cosmetic grade during the run. OQC confirms outgoing batch against signed golden sample and shipment report requirements. Align PO scope with quality and compliance and bowl quality control guide.
Mixer bowl programs · Deep drawing · Ramp planning discussion
Applying this guide in your sourcing workflow
For volume ramp planning for stand mixer bowl oem programs, define the acceptance method and record owner before the part reaches the next gate. Integrate these practices into your existing supplier onboarding gate—not as optional reading after tooling payment. Procurement, quality, and engineering should share the same checklist version so commercial quotes, audit notes, and sample approvals reference identical scope assumptions.
For buyers reading volume ramp planning for stand mixer bowl oem programs, use this point to compare supplier evidence before comparing price. For stand mixer bowl programs, hub interface control and cosmetic grading drive more launch risk than minor piece-price differences. Category-focused manufacturers invest in repeat bowl IPQC because daily volume surfaces defect modes early—buyers benefit when audit and RFQ questions target that discipline.
Cross-functional alignment before factory commitment
In volume ramp planning for stand mixer bowl oem programs, apply this DFM check to the actual geometry, material, and trial result rather than to a generic capability claim. Legal should review NDA and tooling exhibits while engineering completes DFM review—not after mold steel is cut. Logistics should confirm incoterms and pack drop requirements before golden sample sign-off so OQC and transit validation match retail expectations.
For volume ramp planning for stand mixer bowl oem programs, separate what the first sample proves from what still needs production-tool validation. Document every gate in a shared project tracker: RFQ complete, NDA executed, audit pass, DFM signed, tooling milestone payments, T1/T2, golden sample, pilot, volume PO. Gaps in tracker visibility cause internal blame when schedules slip.
When to escalate or pause the program
For volume ramp planning for stand mixer bowl oem programs, put the tooling boundary and custody decision in writing before steel or payment is released. Pause tooling payment if audit reveals unlabeled customer molds, missing IQC records, or unwillingness to show production similar to your geometry. Escalate to executive level when repeated hub failures occur without root cause CAPA, or when document bundles repeatedly fail retailer checklist at incoming.
For volume ramp planning for stand mixer bowl oem programs, put the tooling boundary and custody decision in writing before steel or payment is released. Switching suppliers mid-program is costly but cheaper than launching retail with hub fit failures—plan mold custody and transfer before relationship deterioration makes retrieval adversarial.
Factory capability context for bowl OEM buyers
For volume ramp planning for stand mixer bowl oem programs, define the acceptance method and record owner before the part reaches the next gate. When evaluating Dongguan and Guangdong deep drawing suppliers, compare category focus and repeat bowl metrics—not only quoted piece price. Factories running stand mixer bowls daily maintain hub gauges, cosmetic limit samples, and mold PM logs tuned to high-volume output. Luzhenyu's Chashan base (our Dongguan production base) runs project-matched forming presses with stand mixer bowls represent a major share of customer programs, 250,000+ stand mixer bowls produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output produced per year as a reference output, 200+ tooling development references across customer projects, and customer-funded tooling managed under project agreements under project agreements. Quality workflow follows IQC → FAI → IPQC → OQC; certification status and scope should be verified separately. Use this as a benchmark when auditing any shortlisted supplier, then validate with your own drawing.
Related resources: deep drawing, quality and compliance, stand mixer bowl programs, and submit an RFQ.
Linking buyer decisions to production reality
For volume ramp planning for stand mixer bowl oem programs, separate what the first sample proves from what still needs production-tool validation. Procurement decisions on incoterms, payment terms, MOQ tiers, and supplier scorecards only work when connected to engineering gates: DFM feasibility, T1 dimensional reports, golden sample approval, and pilot validation at line speed. Skipping any gate transfers risk to the next phase—tooling disputes become sample delays, sample delays become ramp failures, and ramp failures become retail stockouts with field complaints.
For buyers reading volume ramp planning for stand mixer bowl oem programs, use this point to compare supplier evidence before comparing price. Complete the OEM RFQ checklist and factory audit checklist before committing tooling budget. Pair with internal approval authority for hub fit and cosmetic sign-off so supplier iteration cycles are not lost to buyer-side review backlog.
Frequently asked questions
What output defines successful ramp?
Stable hub PPM, cosmetic yield at target AQL, OTIF on partial releases—not press speed alone.
Can ramp overlap pilot?
Pilot is ramp phase zero—do not skip to full MOQ without pilot go/no-go.
Who owns ramp chart?
Joint—supplier production planner and buyer program manager.
How does mold PM affect OTIF?
Planned PM in low-demand weeks; unplanned wear causes emergency downtime—track punch radius.
Should third-party inspect during ramp?
Optional for first container at volume speed—not only golden sample era.
Send your drawing for DFM review
Even a rough print, target volume, and finish requirement are enough for a go/no-go and next-step reply within one business day.
Typical first response within 1 business day (WhatsApp often faster for Asia/EU time zones).
Explore more